



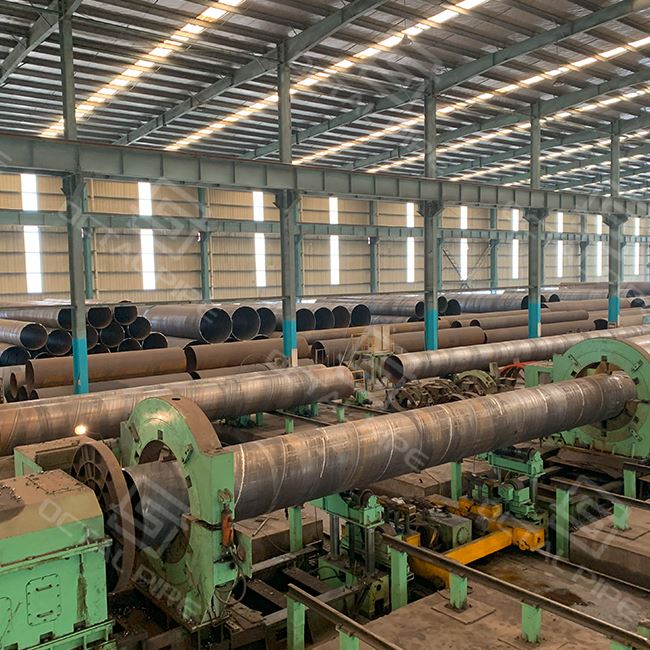
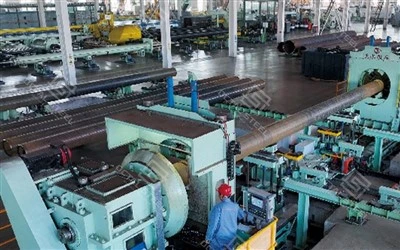
SSAW Pipe Production Line
Inside + outside multi-wire SAW for stable weld quality
Modular Pipe Production Line scope (core + optional modules)
Optional QC: seam tracking, online UT, final UT/RT, hydrotest
Balanced line speed to avoid NDT/testing bottlenecks
Cut-to-length + end facing/beveling for jobsite-ready pipes
For procurement and project engineers, the real value is not "a list of machines," but a matched line where forming speed, welding deposition, NDT throughput, and hydrotest cycle are engineered to work together-so commissioning is faster, weld quality is more stable, and acceptance is easier.
What "Customized" Means in a Real SSAW Pipe Production Line
A "customized" SSAW line shouldn't mean rewriting a brochure-it should mean the line is engineered around three things that affect your ROI directly:
Output & Cost Model
Target annual capacity and shift plan define the right production speed and handling automation.
Standard / Inspection Depth
Your target standard (API/ASTM/EN/GB) and owner requirements determine whether you need online UT only, or online + offline NDT + hydrotest.
Workshop Layout & Logistics
Line layout is matched to your building length/width, crane coverage, coil storage, finished pipe yard flow, and future expansion needs.
What you receive from a proper customization plan
- Process flow + recommended module list
- Layout concept (equipment placement + logistics direction)
- Clear "must-have vs optional" configuration for budget control
- A line that can be upgraded later (automation/inspection/handling)


Typical Technical Parameters
| Item | Typical Range / Notes |
|---|---|
| Line type | Spiral Submerged Arc Welded (SSAW / HSAW) |
| OD range | Typically ~219 mm to 3000+ mm (configured by forming system) |
| Length | Up to 12–18 m (cut-to-length configuration) |
| Welding | Inside + outside multi-wire SAW, matched to target thickness/output |
| Standards | API / ASTM / EN / GB (inspection depth configured to spec) |
| Line mode | Continuous production with synchronized stations |
The point isn't the widest "brochure range." The point is selecting a stable range you can run daily at your target yield.


Process Flow (SSAW Pipe Production Line)
- Coil loading → leveling / edge preparation
- Spiral forming (adjustable angle)
- Inside SAW + outside SAW (multi-wire)
- Online seam tracking + online UT (optional by spec)
- Flying cut-off → end facing & beveling
- Hydrostatic test → final UT/RT (as required)
- Marking, measuring, stacking & dispatch

Customized SSAW Pipe Equipment Configuration
For an SSAW Pipe Production Line, buyers don't just look at "can you weld." They care about stable continuous production, weld seam consistency, and whether the line is configured to meet your acceptance workflow without turning NDT/testing into the bottleneck.
At Octal Pipe, we configure the SSAW line around your OD/thickness window, target standard, and plant layout-so output and quality stay balanced in real production.
1. Coil/Strip Inspection & Traceability (Start Clean, Stay Traceable)
We can integrate coil/strip inspection + traceable marking at the front end, so each pipe can be linked back to raw material and process records.
Why it matters: when owner audits or third-party inspection comes, traceability reduces disputes and speeds up acceptance.
2. Edge Prep That Stabilizes the Spiral Seam
SSAW yield often gets lost at the seam-because strip edge condition drifts. We offer edge milling/trimming options (tolerance level configurable) to keep edge geometry consistent before forming and SAW. Consistent edges improve fit-up and reduce lack-of-fusion repairs during ramp-up.
3. Strip Joining + Accumulator (Continuous Production, Fewer Stops)
To keep the line truly continuous, Octal Pipe can configure strip end shearing + butt welding + accumulator (where required by capacity plan).
Why it matters: fewer line stops = more stable weld parameters and higher real output (not just "theoretical capacity").
4. Spiral Forming With Adjustable Angle (Real Diameter Flexibility)
The forming section is configured with adjustable forming angle and stable roller setup to support your OD range without frequent mechanical rework, diameter flexibility is only valuable if changeover is controlled and repeatable-not "possible on paper."
5. Inside + Outside Multi-Wire SAW (Configured by Thickness & Target Speed)
We configure inside SAW + outside SAW with multi-wire options (wire count and deposition capacity selected by your thickness window and target speed). You want penetration stability and production speed-without having to "slow down to keep quality."
6. Online Seam Tracking + Online UT (Optional by Spec, Not Marketing Add-Ons)
Octal Pipe can integrate seam tracking to keep the welding head aligned with the spiral seam, plus online UT when your spec or customer requires earlier defect detection. It reduces rework and helps stabilize yield during commissioning, especially on large OD and thicker wall.
7. Hydrotest + Final NDT + Finishing (Acceptance-Ready Output)
We configure hydrostatic testing and final NDT depth (UT/RT) as required by your acceptance level, and match it to line speed so QA doesn't choke throughput. Finishing can include flying cut-off, end facing & beveling, cleaning, marking, and stacking.
Why it matters: pipes should ship jobsite-ready, with inspection scope that matches the contract-not a patchwork of add-ons later.


SSAW Pipe Production Line vs LSAW Pipe Production Line
Most buyers don't need a long comparison-they need a decision shortcut.
| Decision factor | SSAW Pipe Production Line | LSAW Pipe Production Line |
|---|---|---|
| Feedstock | Coil / strip | Plate |
| Production mode | Continuous | Step-based forming |
| Strength of choice | High output, flexible OD window, cost efficiency | Often chosen for very demanding project requirements |
| Typical buyer motive | Optimize cost/ton + capacity | Optimize high-end compliance path |
Practical rule:
If your project is driven by volume + flexible OD → SSAW is usually the faster ROI path.
If your project is driven by very strict performance/owner requirements → LSAW may be preferred.

Common Problem
Q1: What is an SSAW Pipe Production Line?
A: An SSAW Pipe Production Line is a continuous system that forms steel coil into a spiral pipe and welds the seam using submerged arc welding to produce large-diameter welded pipes.
Q2: What pipe diameter range can an SSAW Pipe Production Line produce?
A: The OD range is customizable and mainly depends on the forming unit (forming angle) and the welding/handling configuration.
Q3: What equipment is included in a typical SSAW Pipe Production Line?
A: A typical line includes coil loading & leveling, edge preparation, spiral forming, inside/outside SAW welding, cut-to-length, end finishing, and optional inspection/testing modules.
Q4: What information does Octal Pipe need to quote a customized SSAW line?
A: OD & thickness window, target standard, annual capacity/shift plan, required NDT/hydrotest scope, pipe length plan, and workshop layout constraints.
Certifications

CE Certificate

ISO 9001 Certificate

API Q1 Certificate

ABS Certificate

AP-5L Certificate

API-5CT Certificate
| Item | Typical Range (Customizable) |
|---|---|
| Pipe OD | 219–3048 mm |
| Wall Thickness | 5–25.4 mm |
| Pipe Length | 6–18 m (cut-to-length) |
| Raw Material | Steel coil / strip |
| Welding | Inside SAW + Outside SAW, multi-wire optional |
| NDT / Testing | Online UT optional; UT/RT + Hydrotest as required |
| Standards | API / ASTM / EN / GB (by project) |
| Main Production Equipment | Uncoiler & Leveler, Edge Milling/Trimming, Spiral Forming Mill, Inside/Outside SAW Welding Station, Flying Cut-off, Hydrostatic Test Unit, End Facing & Beveling |
Hot Tags: SSAW Pipe production Line,Pipe production Line,Octal Pipe,spiral pipe production line
Previous
ERW Pipe Production LineYou Might Also Like


Send Inquiry